Engineered Cemented Carbide Stock & Indexable Tooling
Explore our top-tier sintered blanks, scarfing inserts, h6 ground rods, and heavy-duty turning grades fabricated under stringent metallurgical protocols.
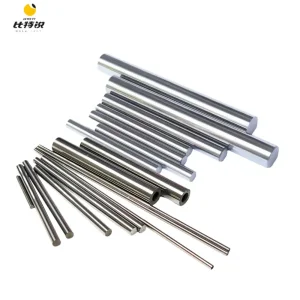
Carbide Rod H6 Ground: Ø1-40mm ultra-fine grain blanks for solid micro drills and high-precision milling tool manufacture.
China Tungsten Carbide Round Rod H6 Ground Ø1-40mm Solid Carbide Blanks Manufacturer, Supplier
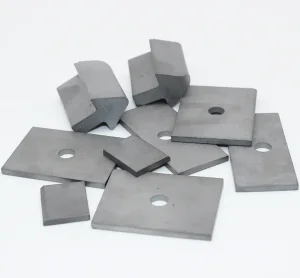
Stone & Wood Cutters: High-impact cemented carbide tips optimized for masonry, quarry saws, and engineered composite timber.
Buy Wholesale sintered cemented carbide stone wood diamond cutting tools Supplier, Factories
Railway Tamping Tips: Patented shock-resistant geometries designed for ballast tamping tines subjected to cyclopean dynamic loads.
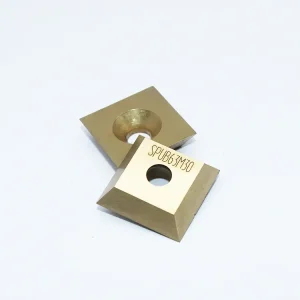
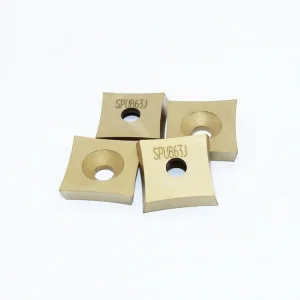
SPUB63M30 Scarfing: TiN-coated longitudinal weld seam trimming inserts for ERW steel tube mills, heat and shear resistant.
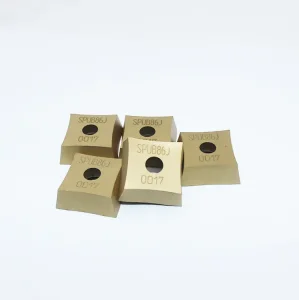
CVD Chuck Jaw Inserts: Wear-hardened clamping and indexable gripping jaws for precision CNC workholding and heavy roughing.
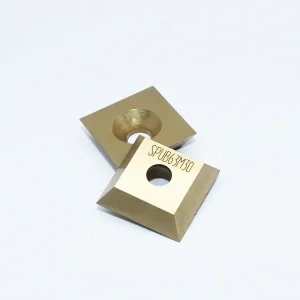
Heavy Lathe Turning: SPUB63 profile turning inserts formulated for roll turning, rough billet sizing, and tough alloy steels.
Buy Wholesale SPUB63 tungsten carbide insert scraps lathe cutting tools turning Supplier, Factories
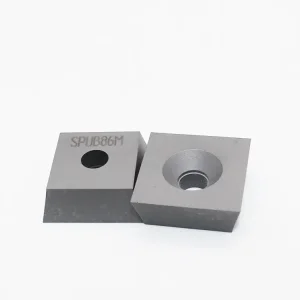
Direct CNC Turning Inserts: ISO standard negative and positive geometry inserts engineered for stable chip-breaking across ISO P, M, and K materials.
Wholesale Factory direct sale tungsten carbide turning inserts Manufacturer, Factory
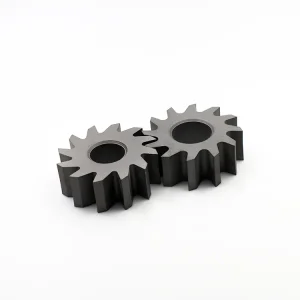
Precision Drive Components: Hardened transmission gears and companion carbide tooling solutions for automated production lines.
Wholesale China best price straight toothed steel small pinion gears Manufacturers, Supplier
Navigating the Global Market for Discount Carbide Inserts
Deconstructing the dichotomy between purchase price and true production cost in modern subtractive manufacturing.
The Myth of "Cheap" vs. The Reality of "Discount"
In high-velocity CNC manufacturing, procuring discount carbide inserts has historically carried an ambivalent reputation. For production managers, inferior inserts sourced from unverified distributors frequently exhibit micro-flaws: micro-cracking from uneven sintering, excessive cobalt leaching, erratic binder distribution, and unpredictable edge chipping. When an indexable insert breaks prematurely, the collateral loss—machine downtime, damaged toolholders, scrapped aerospace or automotive components—instantly obliterates whatever marginal savings were captured on unit price.
Conversely, authentic wholesale discount carbide inserts provided by tier-one Chinese original design manufacturers (ODMs) reflect a structural, supply-chain-driven economy of scale. By capitalizing on regional tungsten mine proximity (Jiangxi province accounts for over half the world’s high-purity wolframite deposits), fully integrated ammonium paratungstate (APT) processing, automated high-tonnage powder press lines, and low unit overhead, factory-direct suppliers offer 35% to 55% lower prices than legacy Western tool brands without sacrificing a single micron of metallurgical purity.
Total Cost of Ownership (TCO) & CPCE Calculation
Industrial procurement departments operating under modern Lean Six Sigma paradigms no longer measure tooling expenditure by invoice item price. The core metric is Cost-Per-Cutting-Edge (CPCE) coupled with Mean Time Between Tool Replacements (MTBTR). The empirical formula governing this operational reality is expressed as:
CPCE = (Insert Purchase Price / Total Usable Edges) + ((Tool Change Downtime × Machine Hourly Burden Rate) / Parts Machined Per Edge)
When factory-direct discount carbide inserts demonstrate edge consistency within a ±0.012mm tolerance band, scrap rates fall to near zero. A discount supplier that provides certified carbide grade chemistry (such as 100% virgin tungsten carbide bonded with cobalt or nickel, devoid of recycled scrap contamination) drives down overall component manufacturing costs by as much as 28% across high-volume production schedules.
Supply-Demand Dynamics & The Evolution of Discount Tooling
Understanding geopolitical resource localization, raw material price fluctuations, and the digital transformation of cutting tool manufacturing.
Upstream Tungsten Concentrate Control
Tungsten (wolfram) has been formally categorized as a critical strategic raw material by both the European Union and the United States Department of Energy. With China controlling over 80% of global tungsten refining capacity, Western tool manufacturers face escalating tariff pressures, complex logistics surcharges, and middlemen markups.
Direct wholesale discount suppliers positioned within Jiangxi's industrial cluster maintain direct upstream access to unadulterated APT (Ammonium Paratungstate). This upstream integration decouples manufacturing from speculative commodity spikes, allowing suppliers to lock in fixed-rate, high-volume contracts for global distribution partners.
Transition to Nanograin & Hybrid Alloys
Modern CNC machining requirements have outpaced traditional coarse-grained WC-Co alloys. The industry is rapidly adopting ultrafine (0.5–0.8µm) and sub-micron (<0.4µm) carbide substrates. These finer grains drastically increase the surface area between hard WC crystals and ductile cobalt binder, yielding an unprecedented combination of high transverse rupture strength (TRS > 3800 MPa) and elevated hardness (> 92 HRA).
Modern wholesale suppliers synthesize these nano-engineered powders at scale, rendering high-performance grades affordable for mid-tier contract machine shops that previously could not justify top-tier brand premiums.
Disintermediation in Global B2B Commerce
The traditional industrial distribution model required cutting tools to pass through domestic exporters, continental master distributors, regional tool distributors, and local sales agents. Every intermediary tacked on a 15% to 30% margin, resulting in an indexable insert that left the press at $1.80 costing an end user $14.50.
Digital supply chain integration, digital CAD-to-sinter quoting, and direct air freight have enabled machine shops, tube mills, and mining contractors in North America, Europe, and Australia to partner directly with Chinese manufacturers, unlocking genuine discount economics without metallurgical compromises.
China Factory 4.0: Metallurgical Precision & Scalability
A look inside advanced Sinter-HIP facilities, automated multi-axis grinding cells, and strict metallographic quality assurance.
Overpressure Sinter-HIP Furnace Engineering
Standard vacuum sintering often leaves residual microscopic pores (A04/B04 porosity rating), creating focal points for catastrophic fracture under cyclic heavy mechanical shock. Zhongfu Carbide operates state-of-the-art overpressure Sinter-HIP (Hot Isostatic Pressing) furnaces capable of injecting 60 to 100 bar of ultra-pure argon gas at temperatures exceeding 1450°C during the liquid phase.
This immense uniform hydrostatic pressure compresses any residual micropores to absolute near-zero porosity (A00/B00 class). The result is a fully dense, pore-free cemented carbide matrix exhibiting optimal fracture toughness, eliminating random blade cleavage during heavy intermittent cuts on cast iron and forged steel workpieces.
- Zero-porosity matrix prevents unexpected internal micro-fissures.
- Guaranteed batch-to-batch magnetic saturation (Cobalt phase validation).
- Superior surface integrity crucial for high-adhesion PVD/CVD film deposition.
Robotic Perimeter Grinding & Nanometer Edge Honing
The performance of an indexable insert is profoundly dictated by the condition of its cutting edge (micro-geometry). Wholesale inserts must adhere to strict dimensional tolerances (ISO classes G, M, and E). Our automated 5-axis CNC periphery grinding centers run continuous diamond wheel passes with real-time in-line laser measurement compensation.
Furthermore, custom robotic brush and drag-finishing stations apply precise micro-hone radii (K-factor controlled between 25µm and 60µm depending on whether the insert is destined for superalloy aerospace turning or high-speed aluminum finishing). Proper edge preparation prevents premature micro-flaking and extends tool life by up to 40% under high chip loads.
- Tight ISO tolerance conformity across edge thickness and inscribed circle (IC).
- Predictable chip curl and evacuation via custom CAD/CAM chipbreaker design.
- Repeatable indexing: less than ±0.008mm variance across 10,000-piece production lots.
Advanced PVD/CVD Nanocoatings & Metallurgical Substrates
Balancing thermal barrier performance, chemical inertness, and lubricity to defeat crater and flank wear.
PVD AlTiN & TiAlSiN Nanocomposite
Physical Vapor Deposition (PVD) operates at lower coating temperatures (450°C–500°C), preserving the substrate's intrinsic toughness without inducing brittle eta-phase formation. Our AlTiN and multi-layer TiAlSiN coatings form an aluminum oxide passivation layer when the cutting edge encounters cutting zone temperatures up to 1050°C.
This barrier is ideal for milling cutters, threading inserts, and interrupted turning operations across austenitic stainless steels (304/316) and heat-resistant superalloys (Inconel 718, Titanium Gr.5).
CVD Multi-Layer: TiCN + α-Al₂O₃ + TiN
Chemical Vapor Deposition (CVD) yields thick (8–18µm), highly wear-resistant coatings engineered for continuous, high-speed turning of alloy steels and gray cast irons. Medium-Temperature CVD (MT-CVD) TiCN provides columnar grain structures that resist abrasive flank wear.
The subsequent alpha-alumina (α-Al₂O₃) layer forms an impenetrable thermal barrier against crater wear caused by scorching chip flow. The final outer gold TiN flash layer serves as a clear visual indicator for operators to assess tool wear and remaining indexes.
Gradient Substrates & Binder Control
A major breakthrough in modern discount carbide inserts is functional gradient sintering. By carefully adjusting nitrogen and carbon activity during high-temperature Sinter-HIP cycles, a cobalt-enriched outer zone (15–30µm thick) is generated right beneath the coating layer.
This ductile cobalt skin provides superior impact absorption, while the underlying core retains lower cobalt and ultra-hard WC grains. This dual-property profile effectively suppresses thermal fatigue cracks (comb cracks) and edge notch failures in heavy interrupted cuts.
Industrial Grade Matrix & Working Parameters
Shortlist your optimal tungsten carbide formulation based on metallurgical binder percentages, physical properties, and workpiece categories.
| Carbide Grade | ISO Range | Binder (Co / Ni %) | Grain Size (µm) | Hardness (HRA) | TRS (MPa) | Primary Industrial Applications |
|---|---|---|---|---|---|---|
| ZF-P10 / YG6X | ISO P05–P15 | 6.0% Co | 0.6–0.8 (Sub-micron) | 91.8 – 92.5 | ≥ 2400 | High-speed finishing of carbon steels, alloy steels, and chilled cast iron tooling. |
| ZF-P25 / YG8 | ISO P20–P30 | 8.0% Co | 1.0–1.4 (Medium) | 89.5 – 90.5 | ≥ 2800 | General turning, semi-roughing, ERW tube scarfing, rock drilling, and brazed lathe tools. |
| ZF-P40 / P40 Class | ISO P35–P45 | 10.0% – 12.0% Co | 1.8–2.5 (Coarse) | 87.5 – 88.8 | ≥ 3200 | Heavy intermittent roughing, roll turning, welded pipe external scarfing (SPUB series). |
| ZF-M20 / TiAlN | ISO M15–M25 | 7.5% Co | 0.5–0.7 (Fine) | 91.0 – 92.0 | ≥ 2900 | Stainless steel turning (304, 316L, Duplex), titanium alloys, medical implant milling. |
| ZF-K15 / Cast Grade | ISO K10–K20 | 6.0% Co | 1.2–1.6 (Medium) | 90.5 – 91.5 | ≥ 2600 | Gray iron, ductile iron, automotive brake disc turning, abrasive non-metallics. |
| ZF-NM10 (Non-Mag) | Specialty | 8.5% Nickel (Ni) | 1.0–1.5 (Corrosion-res.) | 88.5 – 89.8 | ≥ 2200 | MWD/LWD oilfield tools, magnetic sensor housings, subsea valves, non-magnetic dies. |
Engineered Deployment Across Heavy Industrial Sectors
From continuous tube mill lines to railway maintenance and aerospace CNC milling, explore where our wholesale carbide inserts excel.
Steel Pipe Scarfing & Weld Trimming
Electric Resistance Welded (ERW) steel pipe production requires uninterrupted removal of the exterior molten weld bead (scarfing) at velocities exceeding 60 meters per minute. The insert faces searing temperatures, abrasive flash slag, and extreme mechanical chatter.
Our SPUB63, SPUB86, SNMX19, and SNMX25 carbide scarfing inserts utilize tough P40 substrates engineered with specialized convex chip grooves and thick TiN or TiAlN coatings. These inserts resist thermal shock, prevent cratering, and deliver mirror-clean pipe profiles across continuous kilometers of welded tubing.
Railway Track Ballast Maintenance
Railway track tamping machines utilize high-frequency vibrating tines to compact ballast stones underneath cross-ties. The tips of these tamping picks collide with abrasive granite ballast under immense cyclical impact, causing rapid wear on ordinary steel.
Our heavy-duty vacuum-brazed cemented carbide tamping pick tips feature coarse-grain WC-Co composites (9%–12% cobalt) that absorb violent kinetic shocks without fracturing. Field records verify a 400% increase in service life compared to standard hardfaced alloy steel tools.
Aerospace & Defense CNC Roughing
Machining complex aero-structures from Titanium Ti-6Al-4V, 300M high-strength steel, or Inconel 625 generates intense shear heat concentrated at the tool-workpiece interface. Ordinary commercial inserts fail rapidly via notch wear and thermal cracking.
Our ultrafine sub-micron indexable milling inserts (APKT, RDMT, and WNMG geometries) incorporate specialized sharp-edge ground chipbreakers and high-aluminum PVD coatings that deflect heat into the chip, maintaining cutting edge sharpness and preventing work-hardening of the parent aerospace component.
5-Stage Metallographic Verification Protocol
How we eliminate variance and guarantee that every wholesale discount insert delivers consistent batch-to-batch tool life.
Raw Powder Characterization & Fischer Sizing
Every incoming lot of virgin tungsten carbide (WC) and metallic cobalt (Co) or nickel (Ni) binder undergoes strict Fisher Sub-Sieve Sizer (FSSS) particle size distribution analysis, laser diffraction scanning, and inductively coupled plasma (ICP) spectroscopy. We reject any recycled or scrap-adulterated powders to ensure strict grain uniformity before wet ball milling.
- Strict carbon-to-tungsten stoichiometric balance (6.13% wt C).
- Zero trace contamination of deleterious elements (Fe, Ca, S < 50 ppm).
- Precise spray-drying granulation for uniform automated press flowability.
Metallurgical Microstructure & Coercivity Testing
Post-sintered samples from every Sinter-HIP furnace charge are sliced, diamond-polished, and etched for metallographic examination at 1000× magnification under optical and scanning electron microscopes (SEM). We test for eta-phase (carbon deficiency embrittlement) and free graphite (carbon excess porosity).
- Coercivity (Hc): Validates exact grain sizing and grain growth inhibitor performance.
- Magnetic Saturation (4πσ): Confirms exact binder phase chemistry and lack of oxidation.
- Rockwell Hardness (HRA): Multi-point surface testing ensuring complete case depth hardness.
Wholesale Carbide Sourcing Audit Checklist for Procurement Teams
Key criteria industrial buyers must evaluate before approving a high-volume cemented carbide supplier.
1. Virgin vs. Recycled Powder Verification
Require your supplier to provide material composition certificates affirming 100% virgin tungsten powder origin. Recycled zinc-process scrap powder introduces variable grain boundary phases that cause sudden insert fractures in automated CNC cells.
2. Sinter-HIP Furnace Documentation
Always verify that your supplier operates modern pressure Sinter-HIP furnaces rather than low-cost atmospheric vacuum sintering boxes. Sinter-HIP eliminates internal voids and is mandatory for scarfing, mining, and stamping applications.
3. OEM Custom Geometry Prototyping
Evaluate the supplier’s rapid tooling agility. Can they produce custom EDM blanks, special form inserts, or modified scarfing geometries within 15–20 working days? A formulation-driven manufacturer should offer tailored binder mixtures for specific client metallurgy.
Frequently Asked Questions by Industrial Sourcing Managers
Detailed technical answers to common queries regarding pricing structures, coating choices, minimum order quantities, and grade crossovers.
Why are your wholesale discount carbide inserts 30% to 50% lower in price than Western brands?
Our price advantage stems from structural supply-chain integration rather than quality reduction. Located in Nanchang, Jiangxi, our 5,000 m² factory operates directly adjacent to the world's richest primary tungsten reserves. We procure virgin APT directly, eliminate four layers of international distribution middlemen, utilize automated multi-cavity press lines, and operate high-capacity Sinter-HIP furnaces. You are purchasing directly from the source engineering foundry.
How do you guarantee that "discount" inserts will not suffer premature fracture or flaking?
We eliminate premature failure by strictly enforcing 100% virgin tungsten carbide formulations (zero scrap/recycled powder) and processing all blanks through 100-bar overpressure Sinter-HIP furnaces. This closes all micro-porosity to an A00/B00 rating. Every production charge is evaluated for transverse rupture strength (TRS), coercivity, and magnetic saturation, accompanied by a full 3.1 chemical inspection certificate.
Can you provide custom non-standard insert shapes according to 2D/3D CAD drawings?
Yes. Custom manufacturing accounts for over 45% of our factory production. Our in-house mold tooling shop manufactures precision powder pressing dies, and our multi-axis CNC profile diamond grinding centers can hold edge tolerances within ±0.005mm. We routinely engineer non-standard tube scarfing cutters, specialized clamping jaw inserts, non-magnetic valves, and railway ballast wear tips.
When should I specify CVD coating versus PVD coating for discount indexable inserts?
Specify CVD (Chemical Vapor Deposition) for continuous, high-speed, high-heat dry turning and roughing of steel (ISO P) and cast iron (ISO K), where thick TiCN + α-Al₂O₃ layers act as an essential thermal barrier against crater wear. Choose PVD (Physical Vapor Deposition) for interrupted cuts, milling, threading, and machining sticky materials like stainless steel (ISO M) and superalloys (ISO S), where thin, fine-grained, high-adhesion coatings preserve sharp cutting edges without thermal cracking.
What are your Minimum Order Quantities (MOQ) and lead times for wholesale shipments?
For standard catalog geometries (turning inserts, standard scarfing rings, solid carbide round rods), our MOQ is typically 50 to 100 pieces, with stock items shipping within 48 to 72 hours via DHL/FedEx air express. For custom OEM inserts requiring new pressing molds or custom sintering recipes, our initial qualification batch MOQ is 200 to 500 pieces, with prototype samples ready in 15 to 20 working days.
What makes nickel-bonded non-magnetic tungsten carbide distinct from standard cobalt grades?
Standard tungsten carbide utilizes cobalt (Co) as its binder, which is inherently ferromagnetic. In directional drilling (MWD/LWD), magnetic sensor assemblies, or electronic potting molds, magnetic interference ruins signal integrity. We replace cobalt with an advanced nickel-chromium (Ni-Cr) matrix. This renders the material completely non-magnetic (magnetic permeability µ < 1.005) while imparting extraordinary resistance to acidic and saline chemical corrosion.
Heavy Wear Plates, Threading Tools & Specialized Blanks
Expand your tooling program with our heavy stamping die blanks, nano-grain endmill stock, scarfing rings, and precision threaded components.
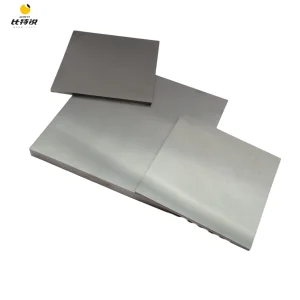
Die Stamping Plate (P30): 200x200x10mm dense HIP-sintered flat stock for heavy sheet metal progressive stamping dies.
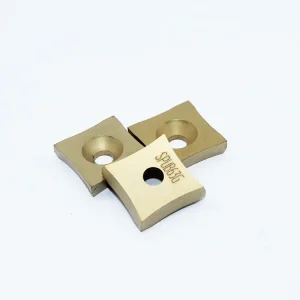
SPUB 63G Threading: Wear-resistant indexable threading inserts configured for oil casing and heavy structural pipe joints.
Wholesale Wear resistant SPUB 63G customize imported carbide threading inserts Factory, Factories
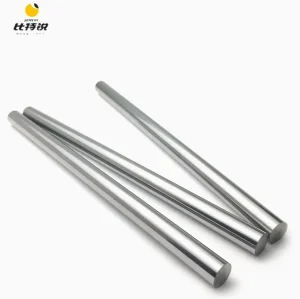
Nano Grain Rods: Ø8 × 330 mm ultra-fine 0.25µm WC blanks engineered for high-rigidity end mills and boring micro-cutters.
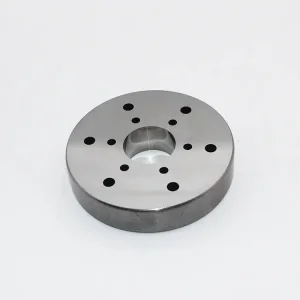
Slurry Pipe Fittings: Custom tungsten carbide-lined elbows, tees, and reducers for severe abrasive petrochemical slurries.
China Customized tungsten carbide fitting elbow tee cap reducer pipe flanges Suppliers, Factories
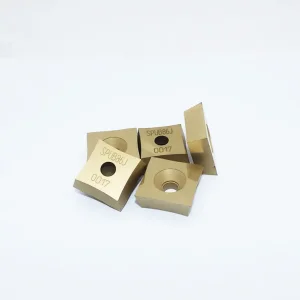
SPUB86J CVD Buttons: Heavy-duty button inserts engineered for industrial woodworking planers and high-load edge trimmers.
Square Thread Tools: High-precision square and acme threading inserts for lead screws, jacks, and power transmission shafts.
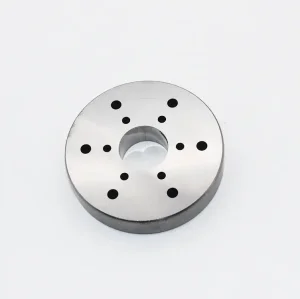
Blind Flange Reducers: Cemented carbide composite blind plates providing extreme erosion resistance in high-pressure piping.
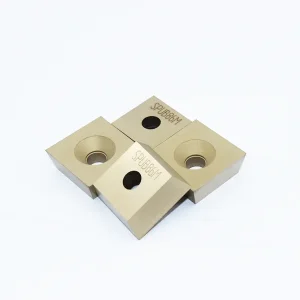
SPUB86 P40 Scarfing: Heavy external tube scarfing inserts designed for structural welded pipe mills requiring extreme edge toughness.
China SPUB86 P40 tungsten carbide scarfing inserts for welded steel pipe Manufacturer, Factory
Request Direct Factory Wholesale Pricing & Custom Grade Trials
Send our metallurgical engineering team your insert geometries, working conditions, or existing tooling part numbers. We will provide a comprehensive Cost-Per-Edge analysis, grade match, and factory-direct wholesale pricing within 8 hours.